English
 French

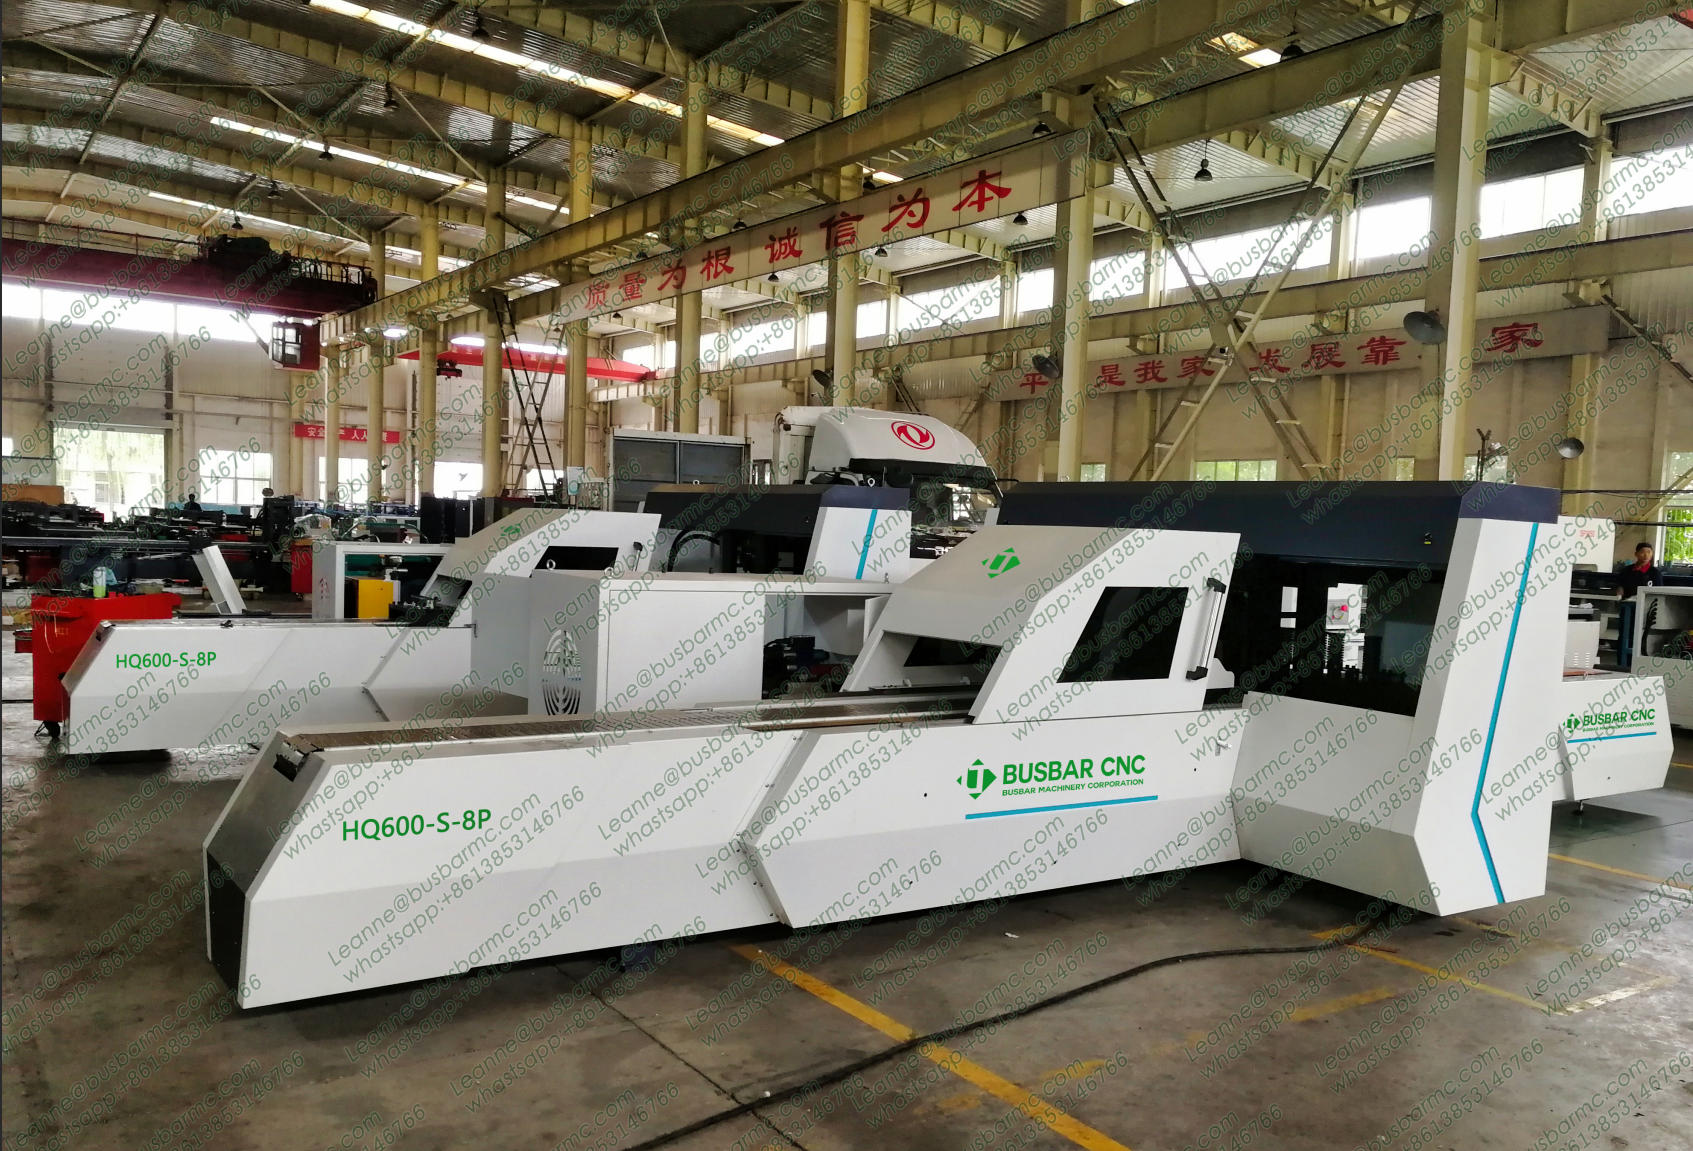
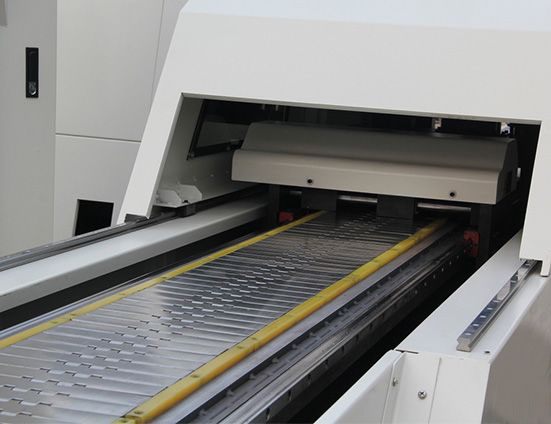
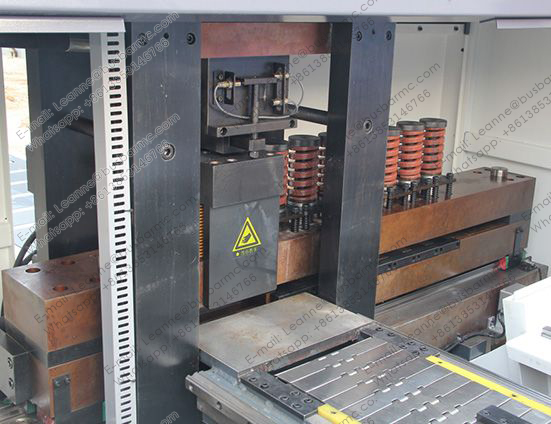
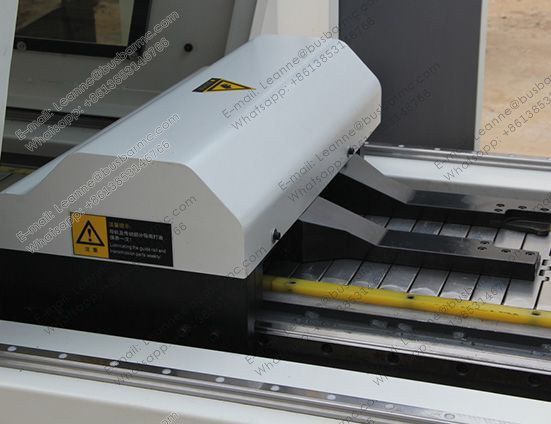
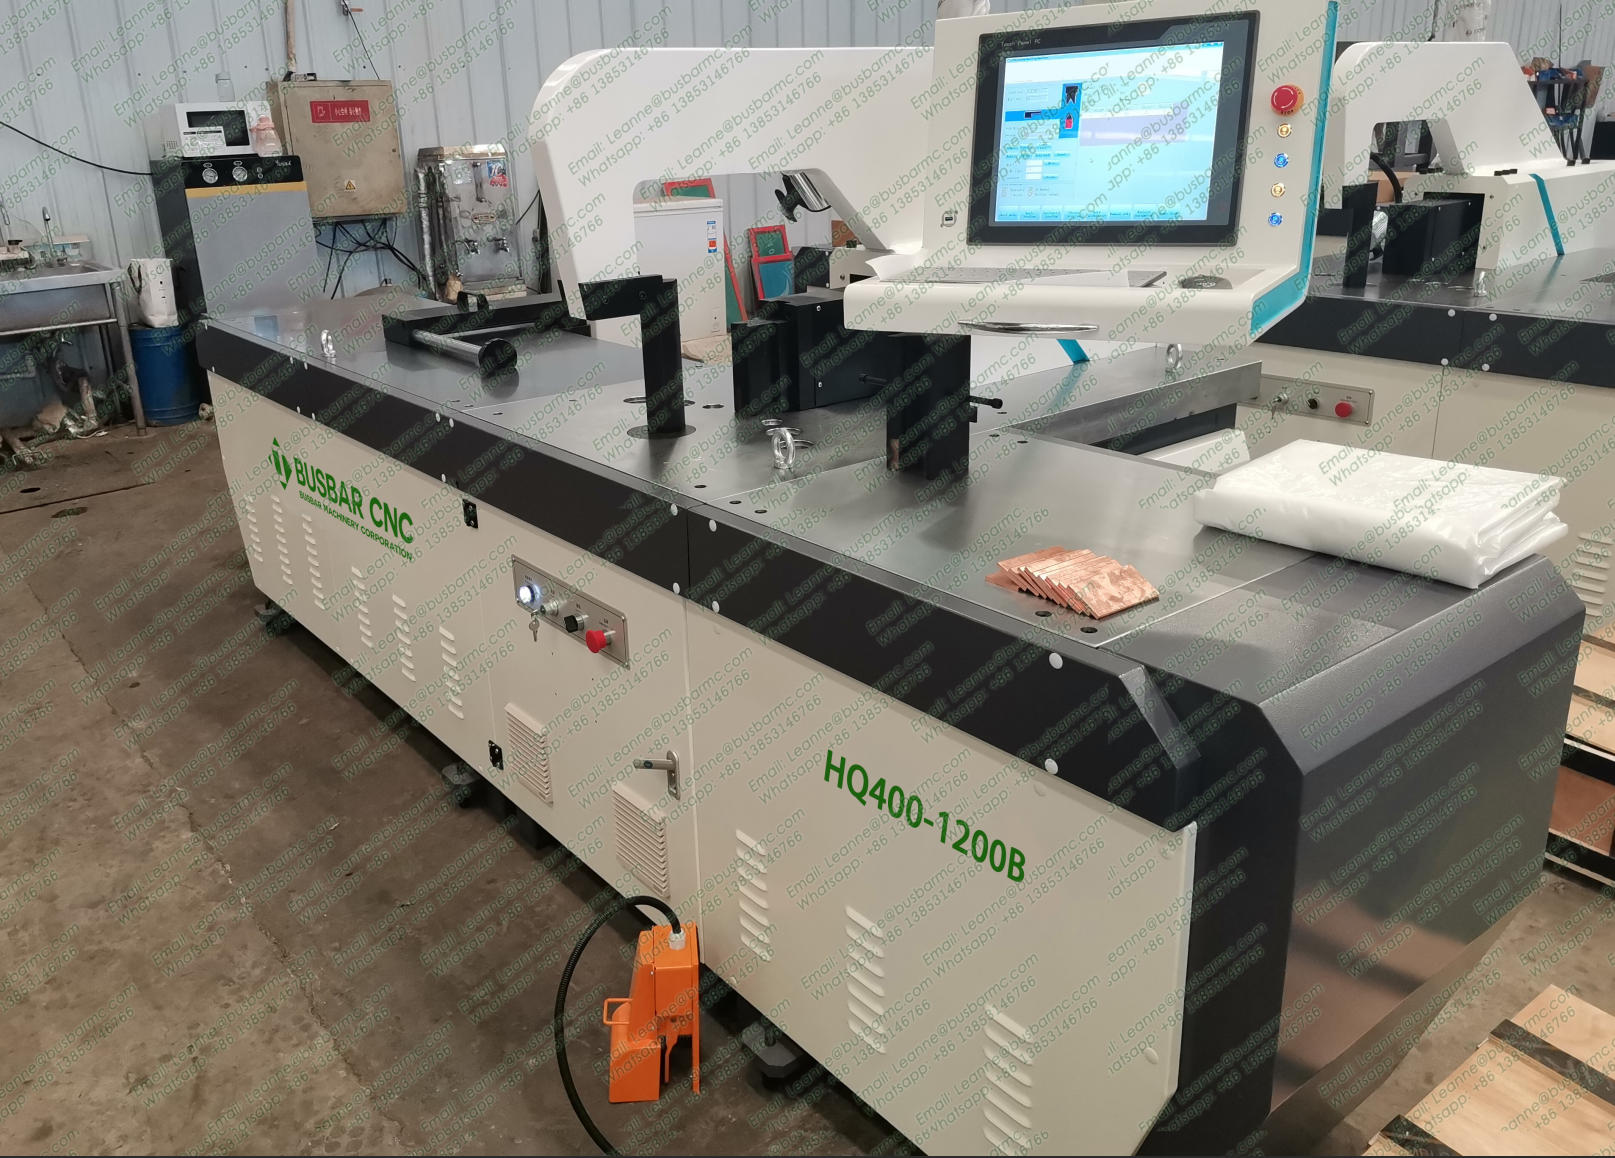
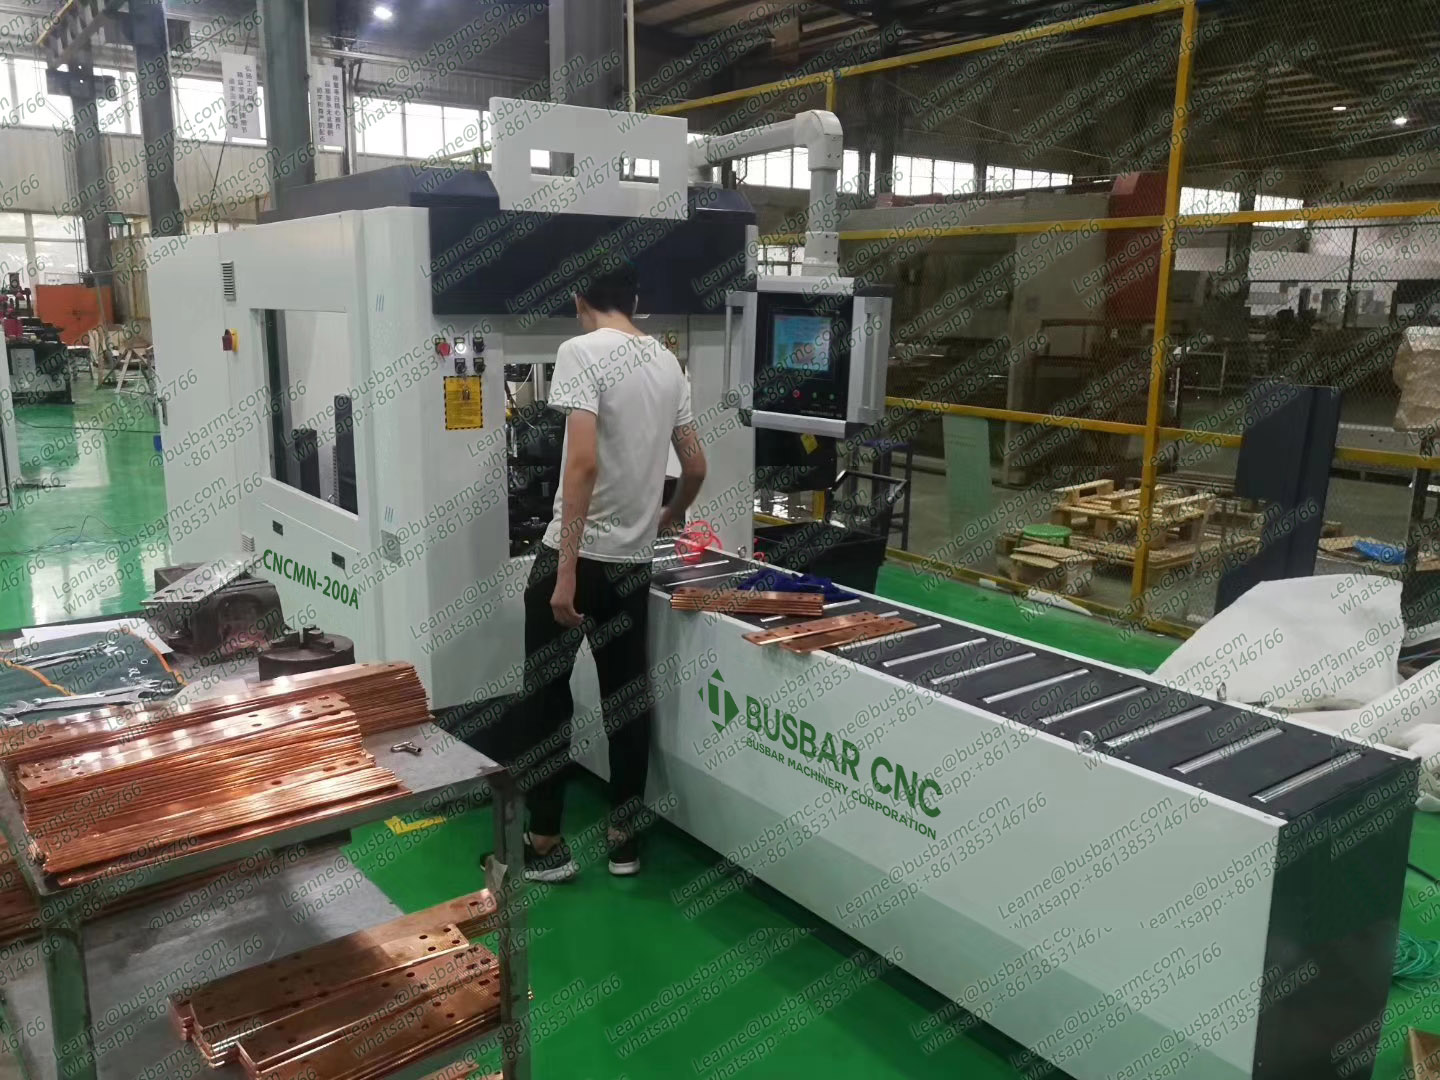
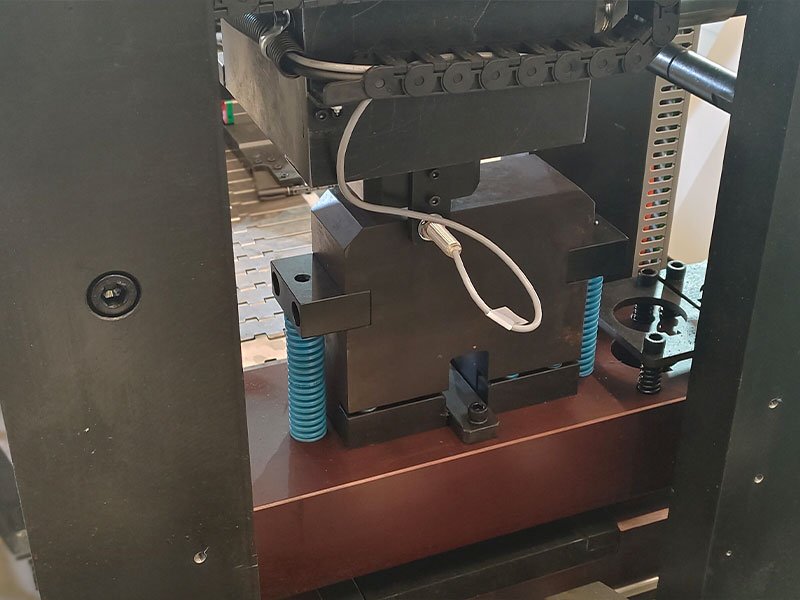
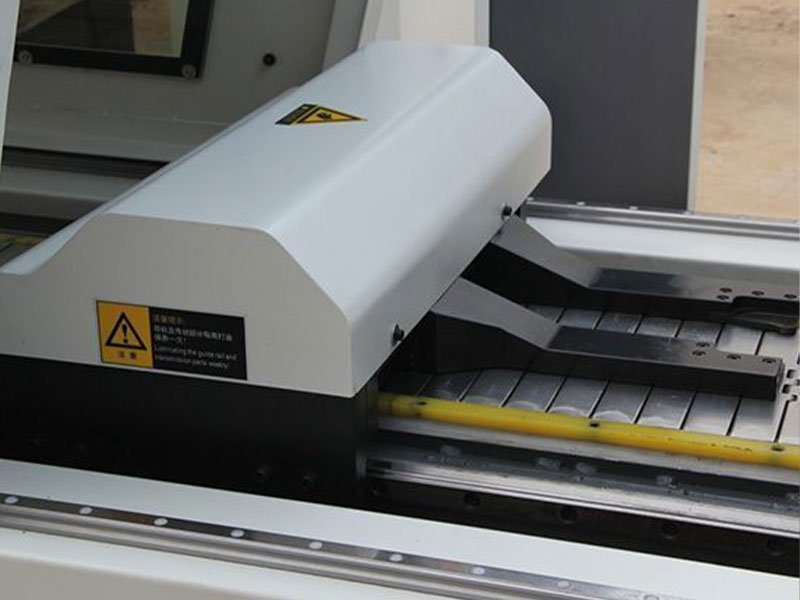
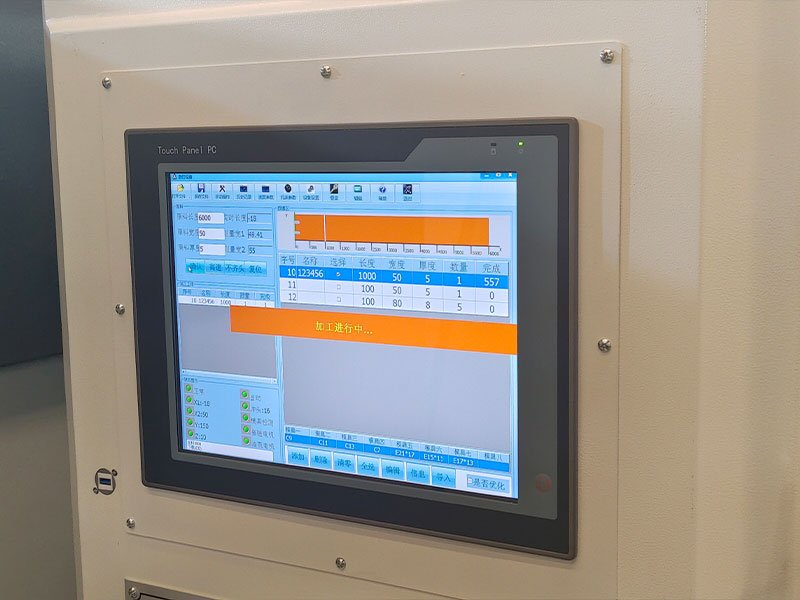
LTMC HQ600-S-8P CNC busbar punching machine is a high-performance CNC busbar processing machine that integratespunching and shearing. TheHQ600-S-8P CNC busbar punching and shearing machine adopts a straight column mold framewith 8 punching,1 shearing to ensure the concentricity of the upper and lower dies during long-term use during processing. It isalso equipped with CNC control system and CAD/CAM system.
The LTMC HQ600-S-8P is a 600 kN CNC busbar punching and shearing machine with an 8-punch + 1-shear inline die library, built for Canadian switchgear and transformer shops fabricating copper and aluminum busbar up to 15 mm thick by 200 mm wide. It processes plates up to 6000×200×15 mm with punching diameters Ø4.3–Ø55 mm and holds 0.10 mm / 500 mm X/Y positioning accuracy across a 6-axis servo system running at 75 m/min. The straight-column single-row die frame keeps upper/lower die concentricity for long-term repeatability, while the Swiss ABB hydraulic motor and German Rexroth/Beckhoff controls suit North American panel shops. At 6700 kg it is a floor-mounted production cell for Ontario and Québec busbar runs.
HQ600-S-8P — Maximum force: 600 kN. Test condition: Swiss ABB hydraulic motor supplying the punching and shearing unit on copper/aluminum busbar. Result: 600 kN nominal hydraulic pressure to the 8-punch + 1-shear station. Baseline: the HQ600-S-7P/8P in family_ref shares 600 kN but lists punching range to Ø35 mm; the HQ600-S-8P extends to Ø55 mm. Canadian shops get full force for 15 mm copper holes.
HQ600-S-8P — Maximum plate size: 6000 × 200 × 15 mm; processing width 200 mm, thickness 15 mm. Test condition: single-clamp long busbar feed, copper or aluminum. Result: 6000×200×15 mm plate capacity, 200 mm width, 15 mm thickness, punching diameter Ø4.3–Ø55 mm. Baseline: the HQ400-S-7P/8P in family_ref is limited to 12×160 mm and Ø4.3–25 mm. The wider 200 mm bar fits 600 V busway risers common in Canadian switchgear.
HQ600-S-8P — Positioning accuracy: 0.10 mm / 500 mm (X and Y); X-axis speed: 75 m/min. Test condition: 6-axis servo motion, X travel 2000 mm, Y travel 960 mm, Z travel 310 mm, processing state. Result: 0.10/500 mm X/Y accuracy, 75 m/min X positioning (150 m/min no-load). Baseline: the HQ400-S-7P/8P in family_ref runs 60 m/min at the same 0.10/500 mm accuracy. Faster feed cuts batch time for Alberta transformer orders.
HQ600-S-8P — Die library: 8 punching dies + 1 shearing die; 6 control axes. Test condition: straight-column single-row die library, 45 mm striking cylinder stroke. Result: 8 punch + 1 shear, 6-axis CNC control, no embossing die (0). Baseline: the HQ600-SP in family_ref offers 7-punch + 1-emboss as an option; the HQ600-S-8P fixes 8+1 for maximum punch count. Ontario shops gain higher hole density per clamp.
HQ600-S-8P — Machine envelope: 10500 × 2750 × 1800 mm; weight 6700 kg. Test condition: installed cell with 3000×500 mm feed and 2500×500 mm discharge stations. Result: 10500×2750×1800 mm footprint, 6700 kg. Baseline: the HQ600-SP line body in family_ref is 10500×2900×1800 mm. Reserve a 2750 mm bay and confirm 600 V / 60 Hz supply with our team.
Yes for North American shops; the servo and hydraulic package (ABB motor, Rexroth servo, Beckhoff control) is specified per order. Confirm your exact supply voltage — 208 V, 480 V or 600 V, 60 Hz — with our team so we match the drive.
Machines ship from the LTMC factory and clear Canadian customs; lead time depends on options and destination port. Request a current quote with Incoterms and estimated transit to your province (Ontario, Québec, Alberta or BC).
The unit uses 8 punch + 1 shear dies with standard punch diameters Ø4.3–Ø55 mm; spare dies, maintenance tools and on-site training are available. Confirm spare-part availability and training with our Canadian contact.
HQ600-S-8P CNC busbar punching machine
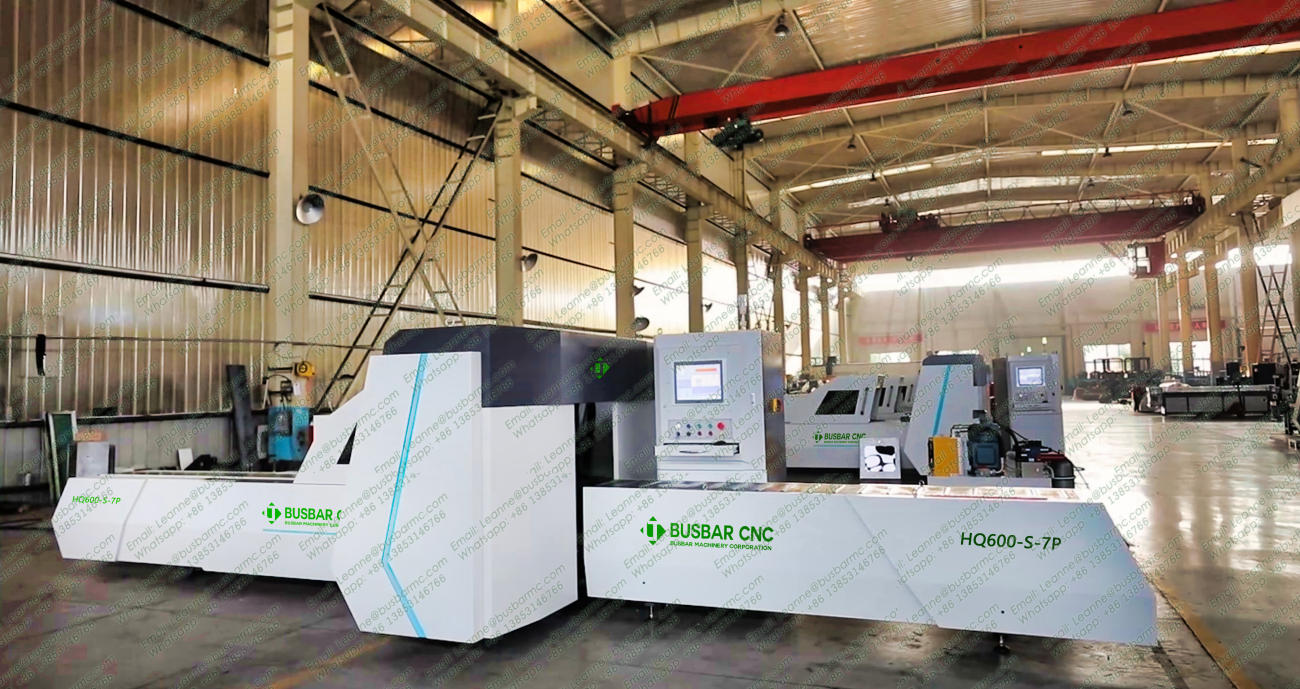
LTMC HQ600-S-8P CNC busbar punching machine is a high-performance CNC busbar processing machine that integrates punching and shearing. The HQ600-S-8P CNC busbar punching and shearing machine adopts a straight column mold frame with 8 punching,1 shearing to ensure the concentricity of the upper and lower dies during long-term use during processing. It is also equipped with CNC control system and CAD/CAM system, which greatly improves the production efficiency of busbar punching and shearing. Get the latest busbar punching and shearing machine prices, contact us now.
LT Busbar Machine Videos:
Infomation:
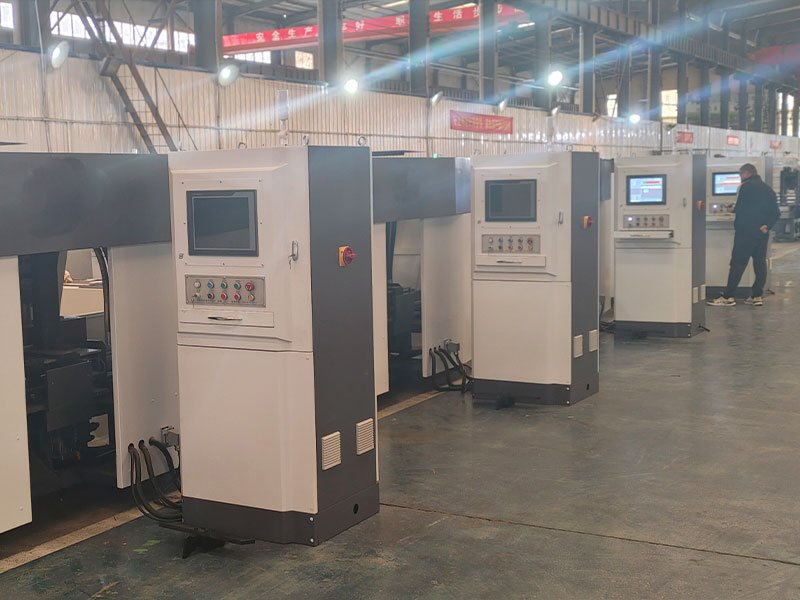
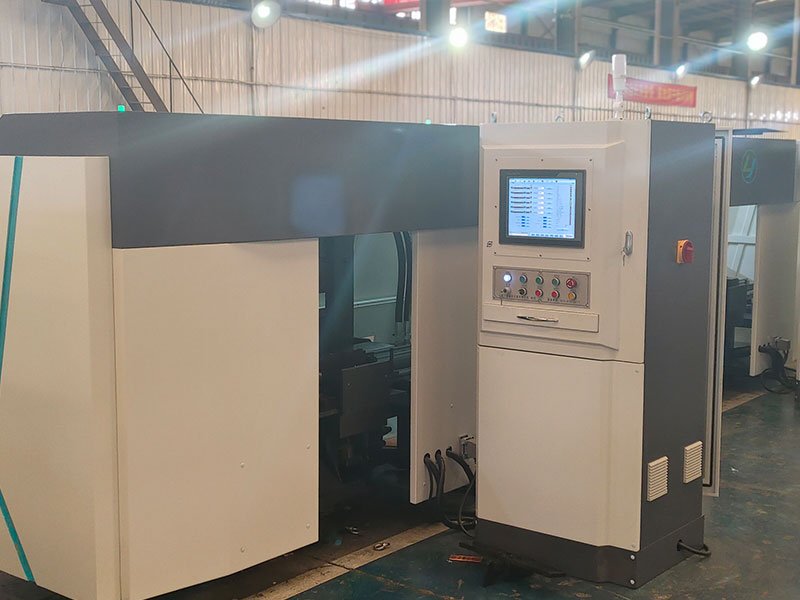
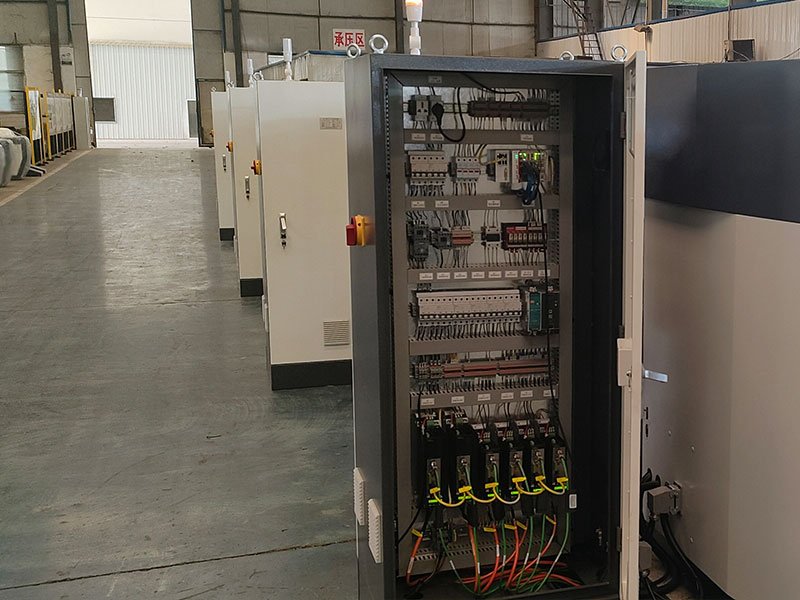
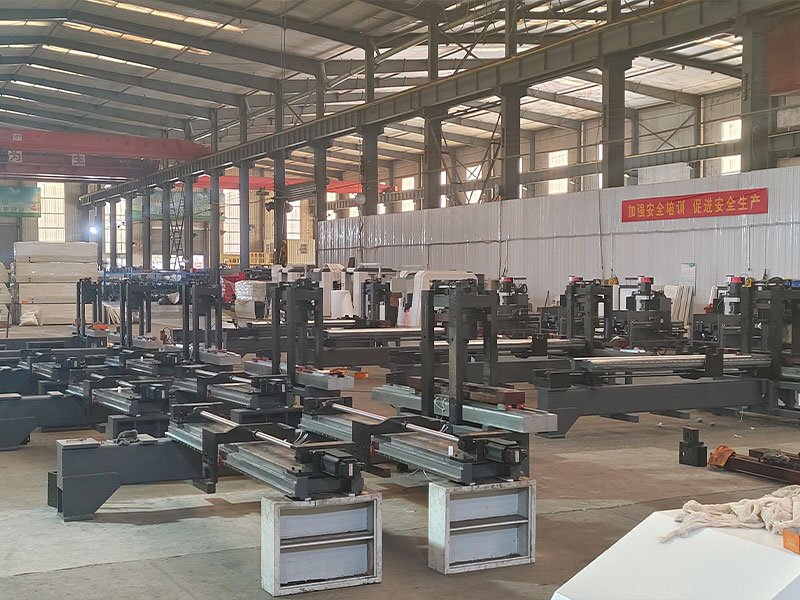
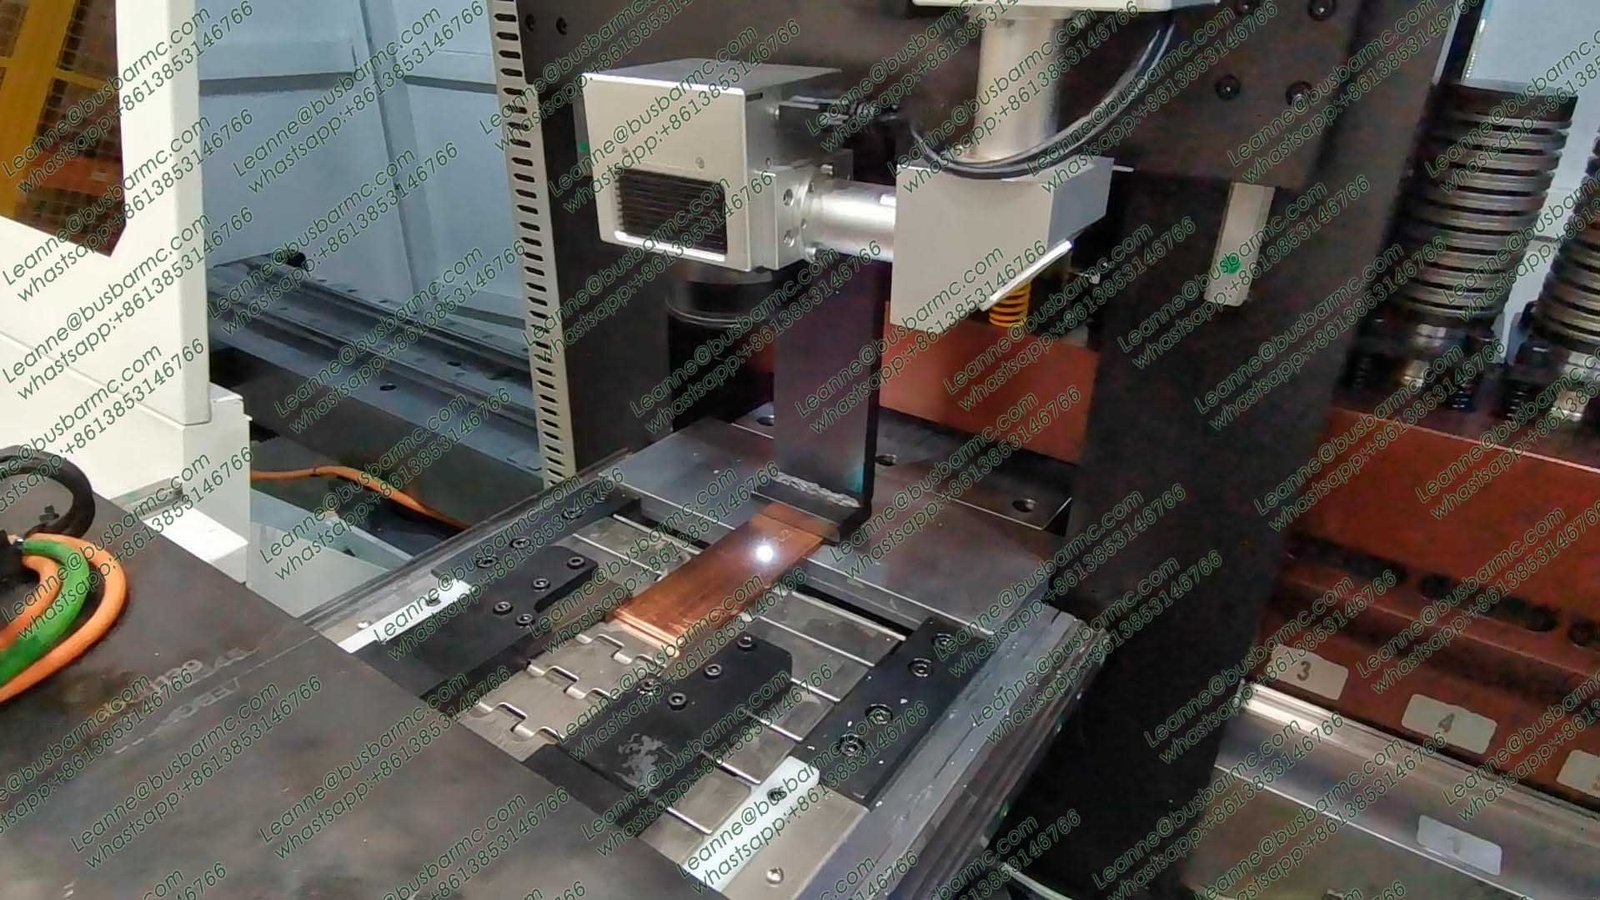
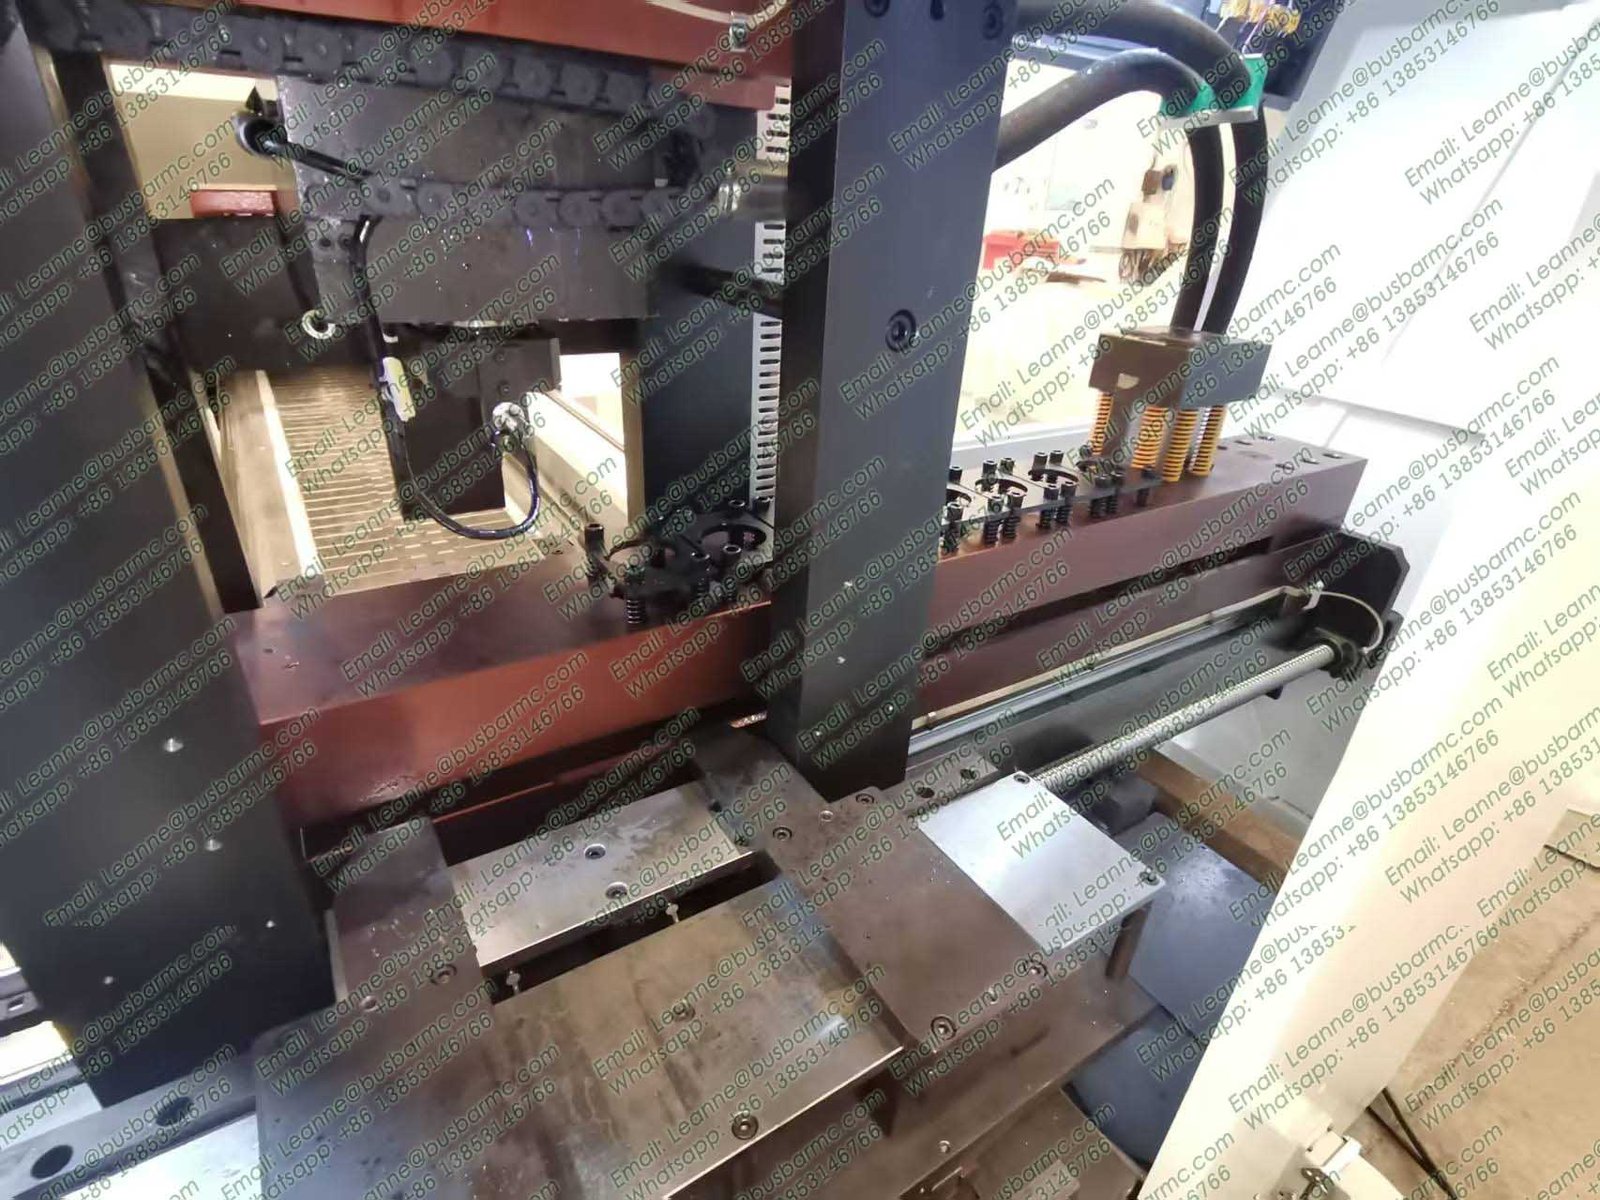
HQ600-S-8P CNC Copper busbar punching machine Specifications
| Model | HQ600-S-8P |
| Maximum Force | 600KN |
| Feeding Station Size | 3000x500mm |
| Discharge Station Size | 2500x500mm |
| Maximum Plate Size | 6000x200x15mm |
| Maximum Processing Thickness | 15mm |
| Maximum Processing Width | 200mm |
| Maximum Punching Diameter | Ø4.3-Ø55mm |
| Maximum Number of Cutting Dies | 1 |
| Maximum Number of Punching Dies | 8 |
| Max.Number of Embossing Mold | 0 |
| X-Axis Maximum Travel | 2000mm |
| X-Axis Accuracy Error | 0.10/500mm |
| Y-Axis Maximum Travel | 960mm |
| Y-Axis Accuracy Error | 0.10/500mm |
| Z-Axis Maximum Travel | 310mm |
| X-Axis Maximum Positioning Speed | 75m/min |
| Striking Cylinder Stroke | 45mm |
| Number of Control Axes | 6 |
| Dimensions (LxWxH) | 10500x2750x1800mm |
| Weight | 6700kg |
Feature:
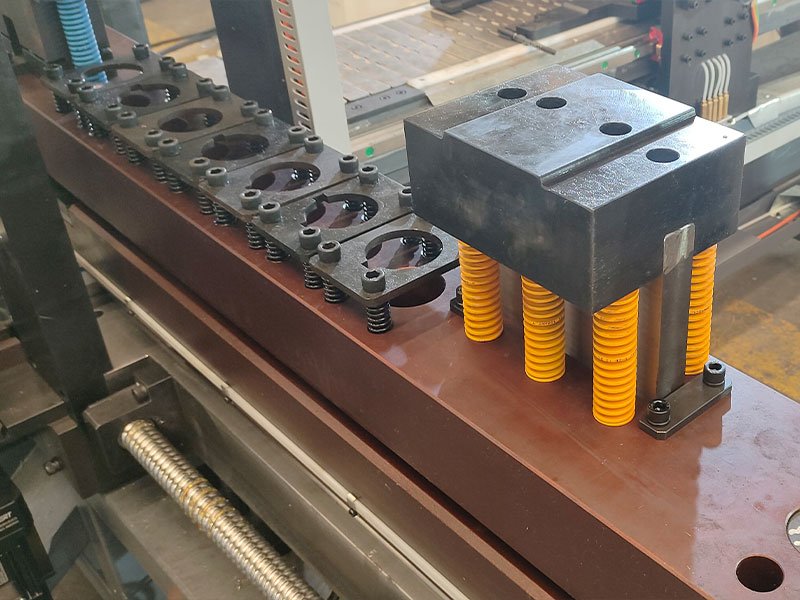
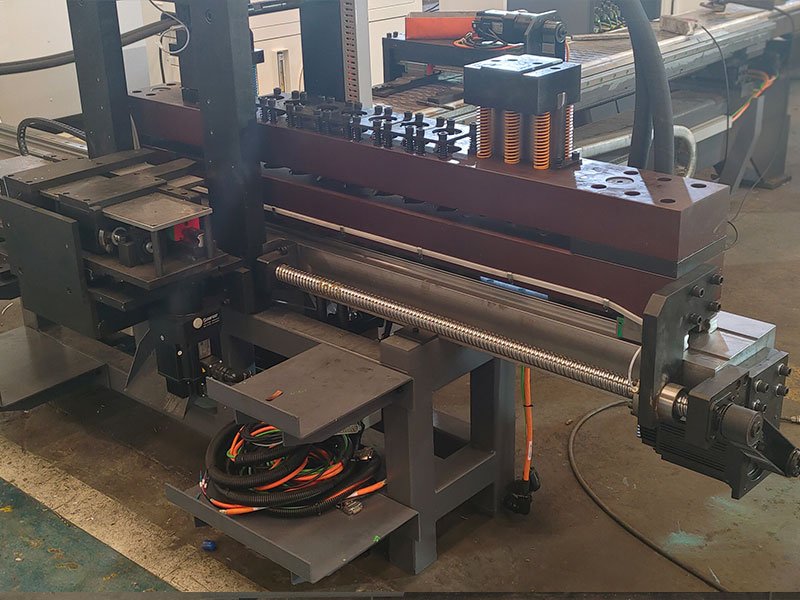
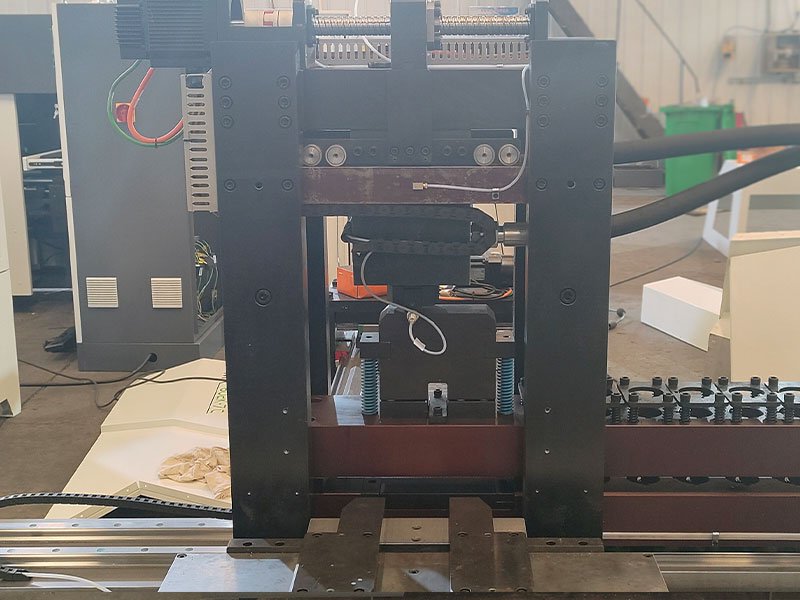
Straight column single row die library, consisting of 8 punching mold + 1 shearing mold .
Single-row die library design, with 8 punching mold + 1 shearing mold in the same row to ensure the concentricity of the punching and shearing work. While ensuring the punching and shearing efficiency (40m/min), the precision control can reach 0.1mm/500mm.
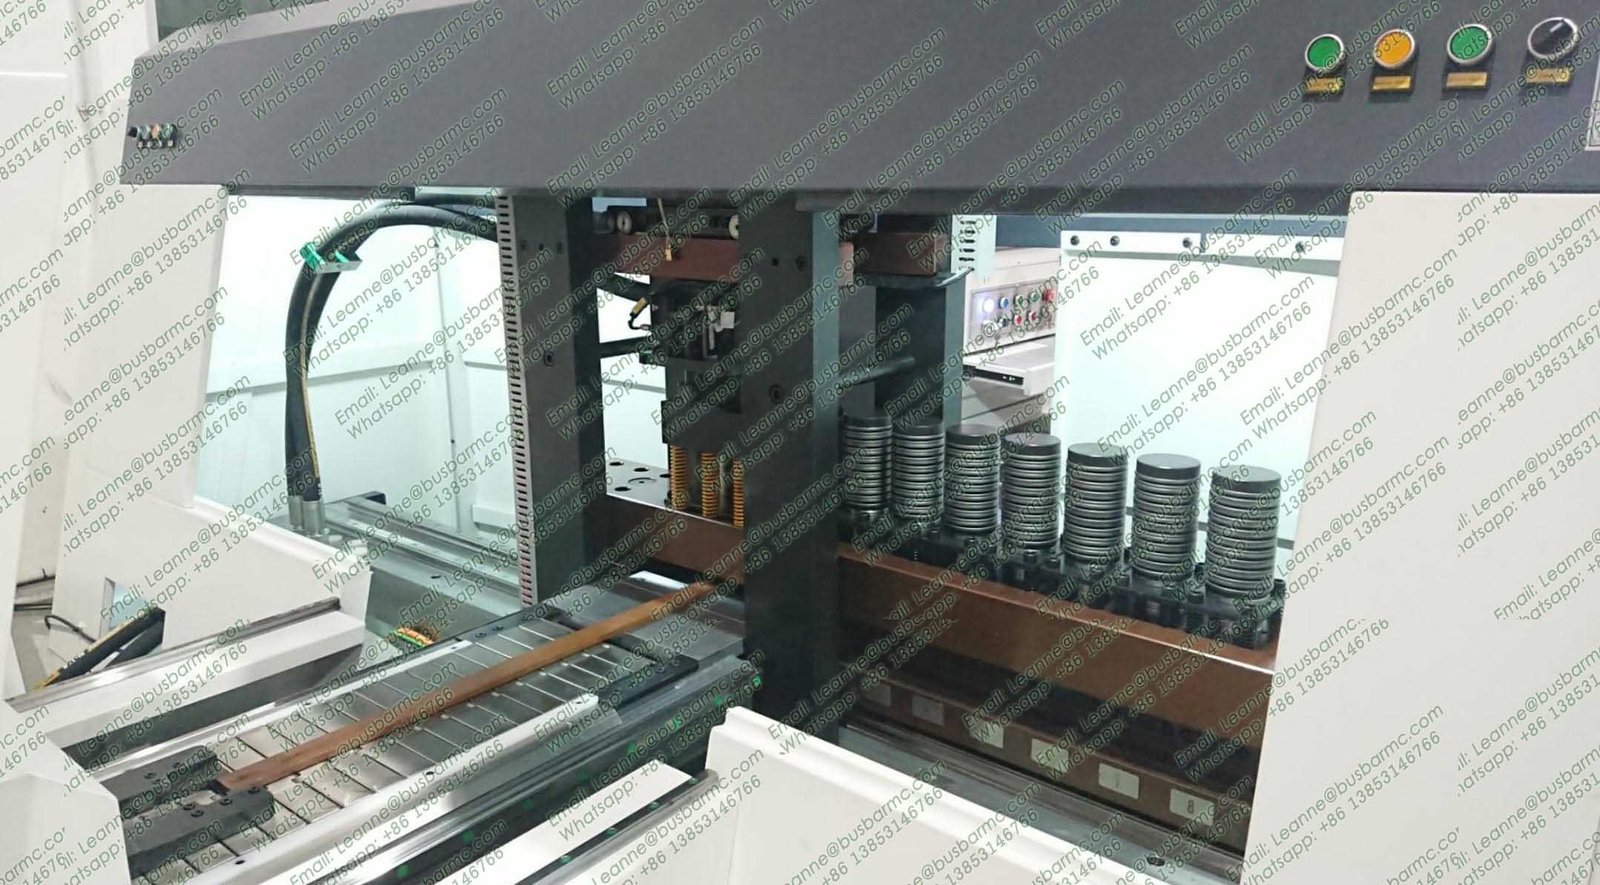
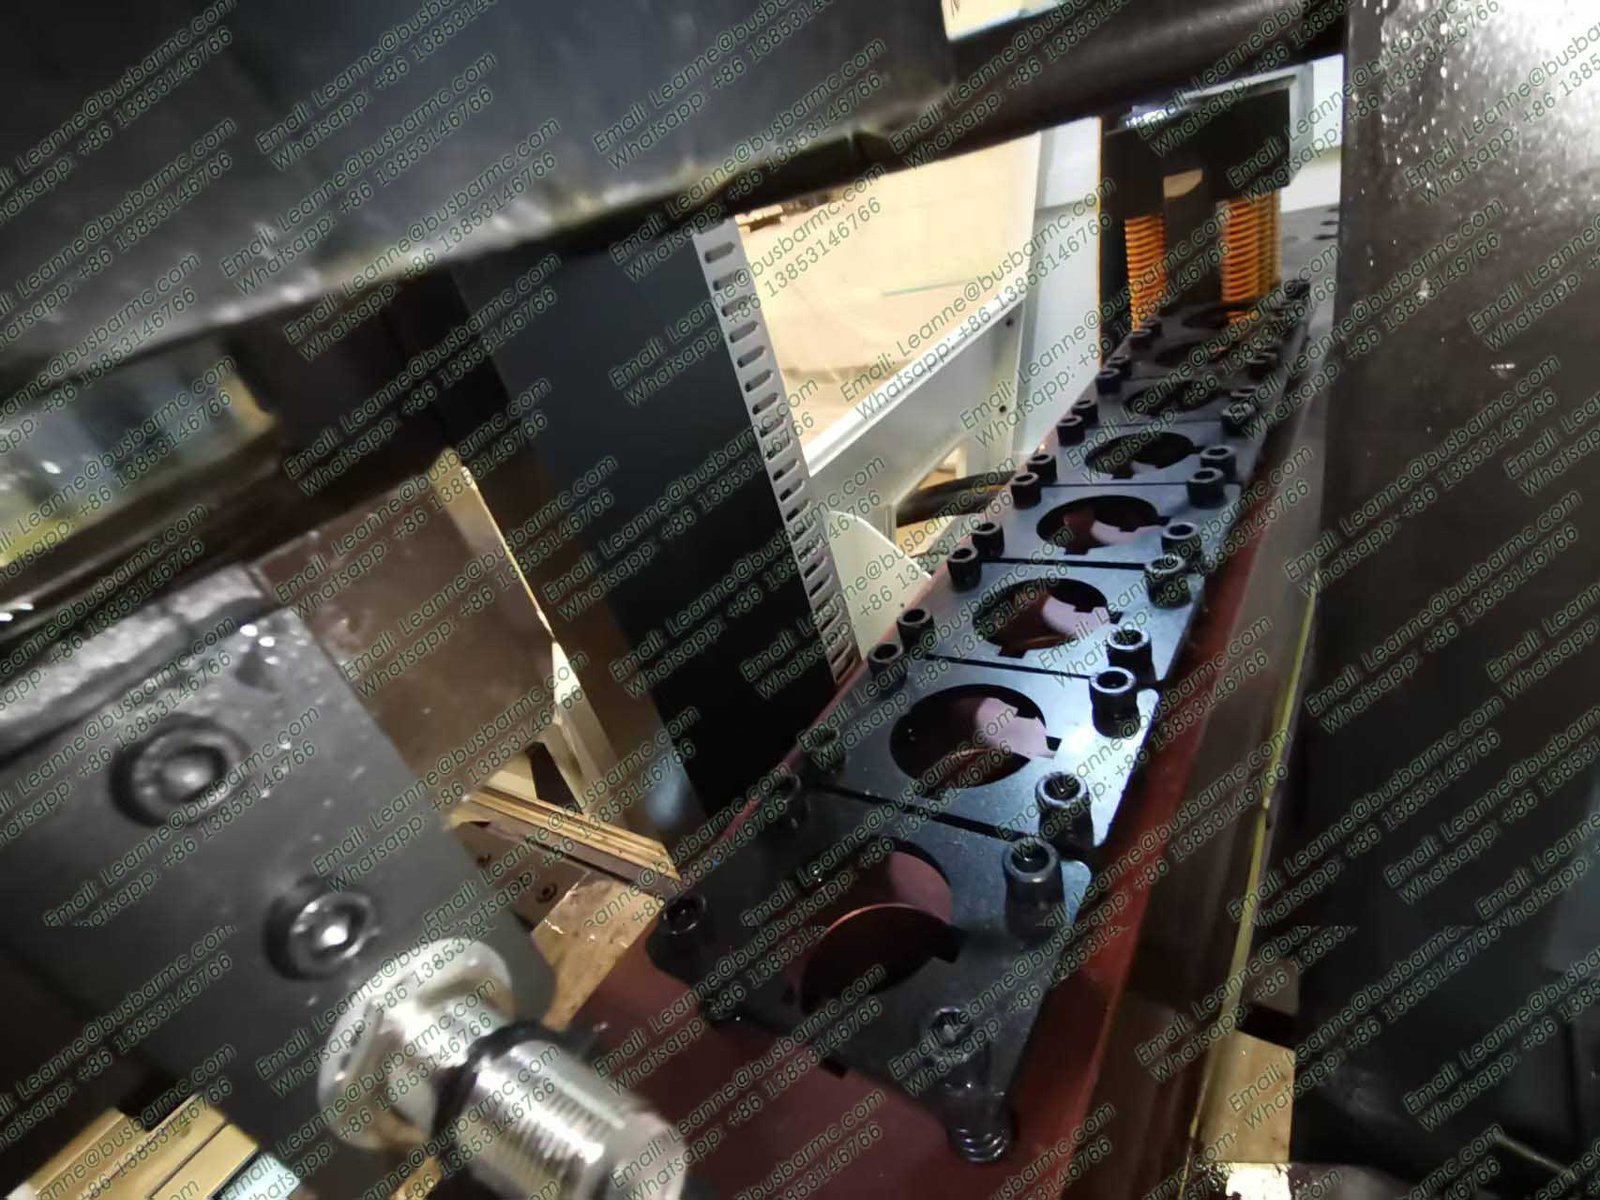
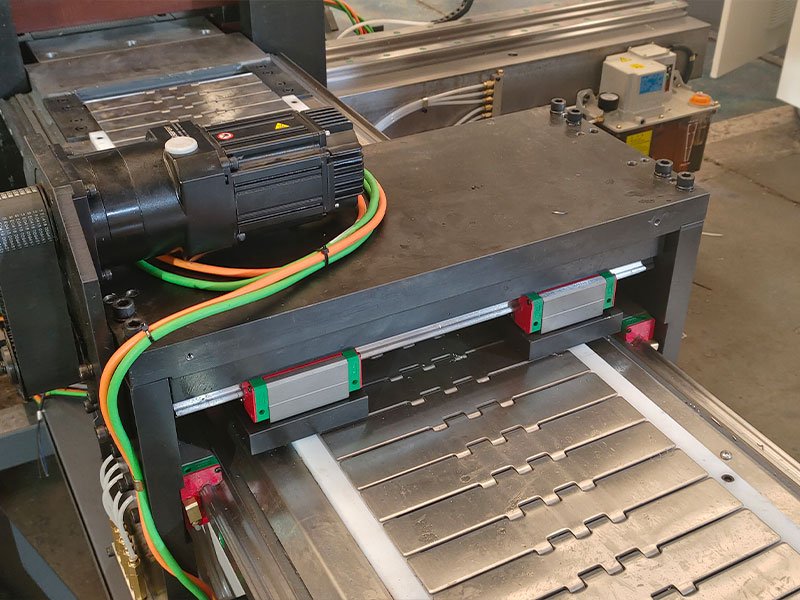
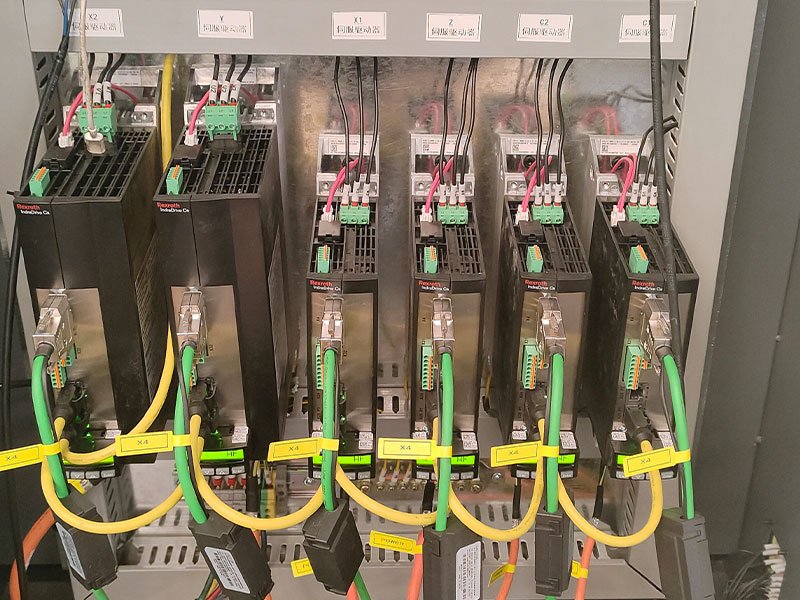
servo system is used to achieve 6-axis control, and the X-axis punching and shearing efficiency is Max 75m/min
6-axis motion system adopts 6 servo servers and 6 servo motors to drive control, with high control accuracy. Among them, the effective stroke
of the X1 servo clamp is 110mm, and the effective stroke of the X2 servo clamp is 2000mm. The X-axis motion efficiency is improved by
shortening the feed stroke and lengthening the discharge stroke. Max 75m/min (150m/min under no-load condition) in the punching
and shearing working state.
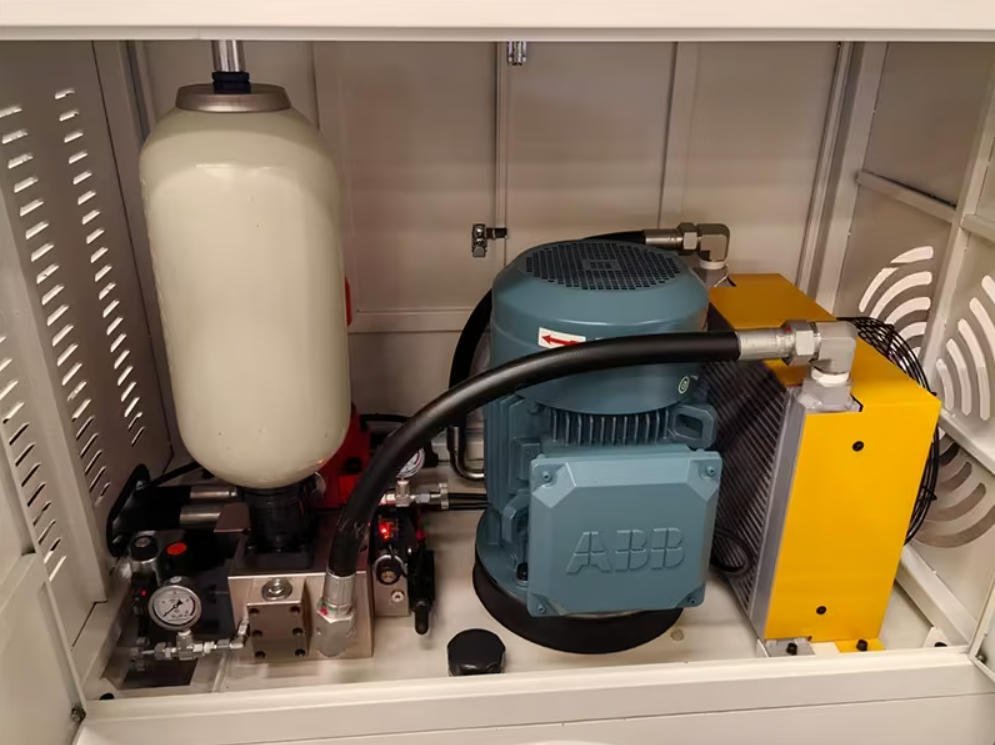
Equipped With A Swiss ABB Motor, It Supplies 600KN Hydraulic Pressure.The hydraulic station uses
Swiss ABB motor to provide 600KN hydraulic pressure, all of which is supplied to the punching and shearing unit,
effectively ensuring sufficient hydraulic pressure and punching and shearing work stability.
German Beckhoff System, German Rexroth Servo Motor And Servo Server.
German Beckhoff control system has closed-loop control, which has the advantages of high control accuracy,
strong anti-interference ability and flexible self-adaptation.
(Siemens control system has poor precision control, adopts open-loop control,
and is prone to data loss.) The equipment uses internationally renowned brand
accessories (German Rexroth), which are more stable than Chinese self-developed
brands and have lower maintenance costs.